


news
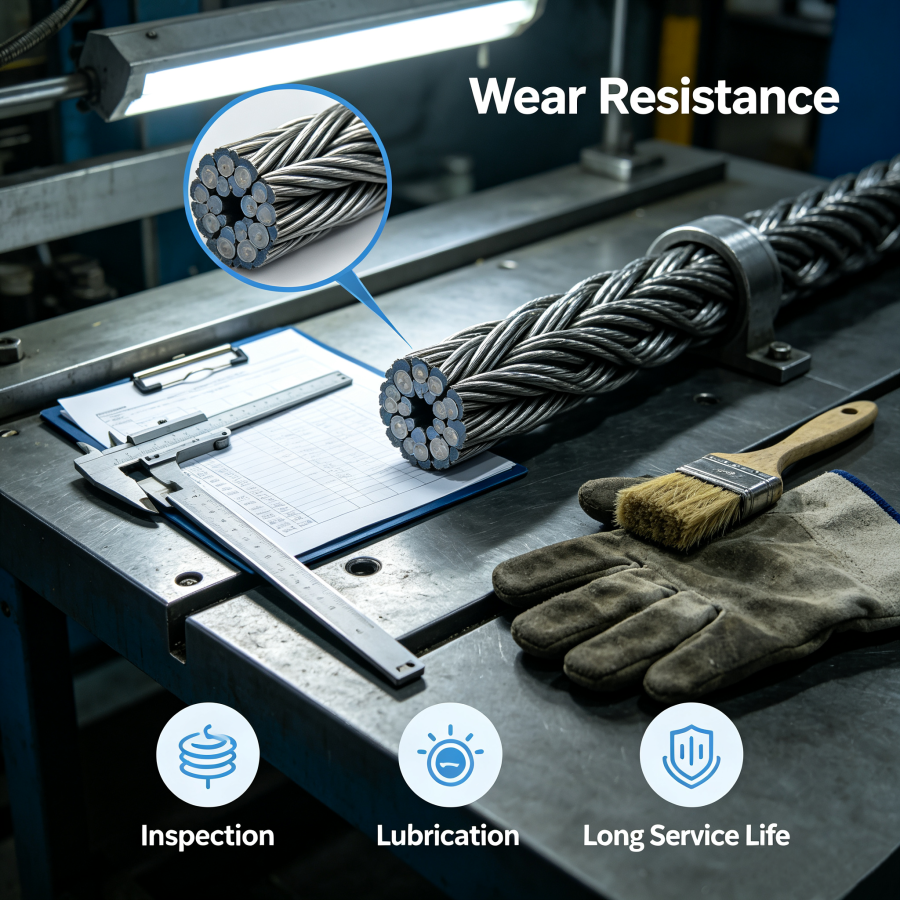
Industrial Wire Rope 101: From Construction to Maintenance
Key Takeaways
- Industrial wire rope is a complex machine made of wires, strands, and a core—not just a simple cable—and each component affects its performance.industrial wire rope
- Selecting the right rope means balancing strength, flexibility, and abrasion resistance while always following the ASME B30 safety factor guidelines for your specific industry.industrial wire rope
- Routine inspection and proper lubrication are not optional extras; they are the two most powerful tools you have to prevent catastrophic failure and extend service life.
- Download our complete inspection checklist at the end of this guide to put this knowledge into action immediately.
What Industrial Wire Rope Is and Why It Matters
Industrial wire rope is the hidden backbone of heavy lifting and load handling.industrial wire rope You see it on towering construction cranes, hear it whirring in elevator shafts, and trust it on ski lifts without a second thought.industrial wire rope At its core, a wire rope is a machine—multiple steel wires twisted into strands, which are then helically laid around a central core. This design isn't just about raw strength; it distributes stress, resists bending fatigue, and provides the redundancy that a solid steel bar or synthetic strap simply cannot offer. When a single wire in a strand eventually fatigues and breaks, the surrounding wires immediately pick up the load without the entire rope failing. This progressive failure mode is deliberate engineering, not a flaw—it buys you the inspection window you need to catch problems before a complete failure occurs. When you need to safely move tons of material hundreds of feet in the air, industrial wire rope remains the only practical choice because it combines high tensile strength with this critical warning system: it rarely snaps without showing visible signs of wear first.
Breaking Down the Anatomy of Industrial Wire Rope
Understanding how a wire rope is put together is the first step toward choosing one wisely.industrial wire rope You cannot evaluate a rope by its diameter alone.industrial wire rope The internal architecture determines whether it will be flexible enough for a small sheave or stiff enough to resist crushing on a multi-layer drum. Think of it this way: a rope that works beautifully on a tower crane with generous sheave diameters might fail catastrophically in just weeks on a tight-sheaved marine winch, simply because the internal wires are being bent beyond their fatigue limits with every cycle. The failure won't look any different from the outside, but underneath, individual wires are snapping one by one.
Wires, Strands, and Cores
Think of the construction in three layers.industrial wire rope First, individual steel wires—available in various grades, with Extra Improved Plow Steel (EIPS) and Extra Extra Improved Plow Steel (EEIPS) being common for high-strength applications—are twisted together to form a strand.industrial wire rope Multiple strands are then wrapped around a central core to form the finished rope. The way these wires are laid up matters immensely. A regular lay rope has wires running in the opposite direction to the strands, giving it good structural stability and making it resistant to unlaying if you accidentally cut a seizing band too early. A lang lay rope runs wires in the same direction as the strands, offering superior abrasion resistance and flexing characteristics because more wire surface area contacts the sheave or drum, distributing wear. But it comes at a real cost: lang lay ropes are far more prone to unlaying and kinking if handled carelessly. You must match this pattern to your sheave size and duty cycle, and you must be honest about whether your crew has the training to handle a lang lay rope safely.
Common Core Materials and Their Impact
The core is the foundation that supports the strands and keeps them in position.industrial wire rope You typically encounter two options: a fiber core (FC) or an independent wire rope core (IWRC).industrial wire rope A fiber core—often made of polypropylene or natural fibers—provides excellent flexibility and acts as a built-in lubricant reservoir. It's a solid choice for hoisting applications with standard-duty cycles, such as a maintenance crane that runs a few lifts per day. However, if you are working in extreme heat or subjecting the rope to heavy crushing forces on a winch drum, you need an IWRC. Here's why: when a rope spools onto a drum under tension, the bottom layers experience enormous compressive forces. A fiber core under that pressure compresses and deforms, allowing the strands to shift out of position and rub against each other. The result is internal wear you cannot see from the outside. An independent wire rope core is essentially a smaller wire rope inside the main rope. It dramatically increases crushing resistance and adds about 11% to the breaking strength, making it mandatory for heavy construction and marine hoisting. Sacrificing an IWRC for a cheaper fiber core in a high-pressure environment almost guarantees premature failure—you'll see the rope lose diameter and go "soft" within weeks, and by then the damage is already done.
Types of Industrial Wire Rope and Where They Excel
Walk into any rigging shop, and the inventory can feel overwhelming.industrial wire rope You will see designations like 6x19, 8x19, and 19x7.industrial wire rope These numbers aren't random; they describe the construction and directly predict the rope's behavior. Narrowing down the type helps you ignore 90% of the catalog and focus on what actually works. The key is understanding that no rope excels at everything. A rope optimized for abrasion resistance will be stiff; a rope optimized for flexibility will sacrifice some wear life. Your job is to identify which failure mode will hit you first on your specific equipment.
6x19 and 6x36 Class: The Workhorses
The 6x19 class (which includes actual constructions like 6x25 filler wire) is your standard hoisting rope.industrial wire rope It consists of six strands with a relatively large number of larger-diameter wires per strand—usually around 19 to 26.industrial wire rope This gives it fantastic abrasion resistance because the thick wires can wear down longer before breaking. You want this on a crawler crane boom hoist or a bulldozer winch where the rope gets dragged through dirt and rock. Its downside is stiffness; it doesn't like small-diameter sheaves. If you force a 6x19 class rope around a sheave that is too small for its construction, the outer wires experience bending stresses beyond their design limit. You won't see a dramatic failure on day one, but microscopic cracks will begin forming in the wires at the bend points, and after a few thousand cycles, those cracks will propagate into full breaks.
The 6x36 class (including 6x37) is the flexible alternative.industrial wire rope These ropes pack many smaller-diameter wires into each strand. The result is a rope that bends around sheaves and drums far more gracefully without fatiguing as quickly. You should reach for a 6x36 class rope on a mobile crane with multiple parts of line or a dockside container crane that cycles constantly. In these settings, bending fatigue kills ropes faster than abrasion, and the flexibility of the 6x36 class directly extends service life. Imagine a dockside crane that moves a container every three minutes, around the clock. That is 480 cycles per day, and every single cycle bends the rope around the head sheave. A stiff 6x19 rope in that application might start showing fatigue breaks in months. A proper 6x36, however, is designed to absorb millions of those bend cycles. The upfront cost difference is real, but the extended service life more than justifies it.
Rotation-Resistant and Specialty Ropes
If you are lifting a heavy load with a single-part line—meaning the load is free to spin—a standard rope will unlay and potentially cause a catastrophic rotational failure.industrial wire rope This is not theoretical. Picture a tower crane lifting a 20-ton steel beam 300 feet straight up on a single line. A standard 6-strand rope under that load will try to unlay, transferring torque down to the load. The beam starts spinning, slowly at first, then faster as the torque accumulates. In seconds, you have an uncontrolled rotation that endangers everyone on the site and could snap the rope entirely. Rotation-resistant ropes, typically built with 8, 19, or 34 strands in complex layers, are engineered to neutralize torque. The inner strands are laid in one direction while the outer strands are laid in the opposite direction, so the torsional forces cancel each other out. You'll find these essential in mining hoisting, helicopter rescue, and anywhere the load must stay perfectly still. In marine environments, you may also encounter galvanized or stainless steel ropes for corrosion protection, or compacted strand ropes that are swaged to a smooth surface, reducing drum wear. While these specialty ropes cost more upfront, matching the specialty to the hazard is a direct investment in crew safety.
How to Select the Right Industrial Wire Rope for Your Application
Selection doesn't start with the rope; it starts with the worst-case scenario at your specific jobsite.industrial wire rope Guessing based on what you used last time is a dangerous shortcut. You need to work through the constraints methodically, letting the physical demands of your equipment dictate the spec sheet.
Key Factors: Strength, Flexibility, and Service Life
Your absolute non-negotiable is breaking strength.industrial wire rope You must calculate the maximum load the rope will ever see, including dynamic shock loads from sudden stops, and then apply the design factor. For most overhead hoisting under ASME B30 standards, that means the rope's catalog breaking strength must be at least five times the working load limit. A bridge crane in a steel mill, however, might require a design factor of 8:1 due to extreme heat and duty. Once strength is met, pivot to fatigue life. If your system uses a D/d ratio (drum diameter to rope diameter) smaller than 30:1, you have a bending fatigue problem. Abandon the stiff 6x19 class and jump to a 6x36 or even an 8x19 construction to survive the tight bends. Here is a practical example: you have a winch with an 18-inch drum and you need a 3/4-inch rope. Your D/d ratio is 24:1, which is well under the 30:1 threshold where fatigue starts to dominate. A 6x19 rope in this setup will fatigue prematurely. Switch to a 6x36 class, and you'll get markedly longer life from the same equipment.
A Simple Decision Framework Based on Your Industry
To cut through the data sheets, use this logic flow tailored to common industries:
- Mobile Crane & Heavy Construction: You need high strength-to-weight ratios with crush resistance.industrial wire rope Start with an IWRC, 6x36 class, and check whether the boom geometry requires rotation-resistant construction for single-part lifts.
- Shipyard & Offshore: Corrosion is your primary enemy. Start your search with galvanized or stainless ropes, and consider a dense 6x36 construction with a fiber core if the rope is static, or an IWRC if under heavy spooling pressure. One common failure mode here is using an ungalvanized rope in a saltwater environment and assuming you can just grease the outside. Salt spray penetrates the valleys between strands and attacks the inner wires long before you see rust on the surface.
- Mining & Slope Hoisting: Safety is paramount. You need a rotation-resistant rope, likely a 34x7 or 35x7 construction, to prevent payload spinning during the long vertical drop down the shaft wall. Never substitute a standard 6-strand rope here.
- Dockside & Container Handling: Duty cycle is everything. Prioritize bending fatigue resistance above all else. An 8x19 or a high-flex 6x36 with compacted strands will deliver the longest service life despite millions of cycles.
Keeping Your Industrial Wire Rope Safe Through Inspection and Care
Chains rarely give warnings, but wire rope often does—if you are looking.industrial wire rope A formal inspection program transforms a wire rope from a consumable item into a predictable engineering component. Every operator running a hoist should view the rope as a gauge of the machine's health. The difference between a crew that catches retirement criteria early and one that runs ropes to failure is often just a structured checklist and the discipline to use it every single shift.
What to Look For During Routine Inspections
Per the ASME B30 standard, you must establish periodic inspections based on usage.industrial wire rope During a visual check, you are looking for the specific retirement criteria. Count broken wires in one rope lay length. If you find six or more broken wires in a single strand lay, or three in a valley between strands, the rope is typically at its discard point. Look for a reduction in diameter below the manufacturer's nominal limit; severe wear often hides under the surface. Pay extremely close attention to zones near end connections and where the rope interfaces with equalizer sheaves—these are fatigue hot spots. If you see a "birdcage" (where the core fails and strands pop out of alignment), stop the lift immediately. That rope has turned from an asset into a hazard. A common mistake here is only inspecting the visible sections of rope. The portion that sits on the drum or wraps around hidden sheaves experiences the same loads as the exposed sections but rarely gets the same scrutiny. Make it a habit to run the rope through its full travel at least once per week and inspect every inch.
Lubrication and Storage Best Practices
Wire rope lubricants serve two purposes: they fight internal friction between moving strands and they seal the exterior from moisture.industrial wire rope A heavy, penetrating lubricant formulated specifically for wire rope must reach the core. Never rely on grease from a brush alone; applying cold, stiff grease just coats the outside and traps moisture inside. If possible, use a roller coater or a drip system that penetrates while the rope is slightly stretched on a drum. If you must apply by hand, do it on a warm day or warm the lubricant first, and work the rope back and forth to open the strands slightly so the lubricant can seep inward. For storage, keep coils off bare soil and under cover. If you leave a rope in a humid environment without lube, you will get internal pitting that cannot be seen from the outside but will sharply degrade breaking strength. One real-world example: a maintenance yard stored spare hoist ropes on a concrete floor near an open bay door for six months. The ropes looked fine externally, but when they were finally put into service, they failed inspection within weeks. The constant humidity cycling had corroded the internal wires, and the breaking strength was compromised before the rope ever left the drum.
Common Wire Rope Mistakes That Can Cost You
The quickest way to burn through a rope budget is not through hard work; it's through bad habits.industrial wire rope The first, and most dangerous, mistake is using a non-rotation-resistant rope on a free-suspended load without a swivel. When the rope unlays, its strength can drop by 30% instantly, and the live strands become a snagging hazard. The second mistake involves the direction of spooling. If you mount a standard right-lay rope on a right-hand drum, it must start at the right flange. If you flip this, you induce a reverse bend and immediate torquing that opens the rope's lay. To avoid this, always follow the manufacturer's spooling diagram and physically verify the direction before loading the rope onto the drum. A crew in a hurry can waste a brand-new rope in one shift simply by spooling it backward. Finally, the silent killer is lubrication neglect. You cannot hear internal corrosion grinding away the strands, but by the time you see the red rust bleeding through the valleys, the rope is already scrap. Oil your ropes enough to keep the outside slightly tacky to the touch, and never use diesel or crude oil—they wash away the manufacturer's internal compound and provide almost no lubrication.
Putting It All Together: Your Next Steps
You've seen that industrial wire rope isn't a generic commodity.industrial wire rope It's a critical safety system that requires you to match the construction to the lift, follow the ASME discard criteria without hesitation, and protect your investment with correct lubrication. The decisions you make at the purchasing level—choosing between a fiber core and an IWRC, or between a 6x19 and a 6x36—directly determine whether your rope fails at 500 cycles or 5,000 cycles.
To make this practical, we've consolidated the ASME inspection standards and the industry-specific selection framework into a single actionable resource.industrial wire rope
Make this guide work at your facility.industrial wire rope Download the Industrial Wire Rope Selection & Inspection Checklist PDF below to keep a hard copy with your maintenance logs. Bring it to your next pre-shift walkaround, and start seeing your rigging gear through the lens of a trained inspector.
Frequently Asked Questions
When should an industrial wire rope be replaced?
You should replace an industrial wire rope when visual inspection reveals six or more broken wires in a single strand lay, three broken wires in a valley between strands, a measurable diameter reduction below the manufacturer's limit, or any birdcaging where the core fails.industrial wire rope Under ASME B30 standards, you must establish periodic inspections based on usage, paying close attention to fatigue hot spots near end connections and equalizer sheaves.
Which is better for heavy lifting: fiber core or IWRC wire rope?
An Independent Wire Rope Core (IWRC) is the better choice for heavy lifting applications where crushing forces exist, such as multi-layer drum spooling or heavy construction hoisting.industrial wire rope The IWRC adds about 11% more breaking strength and prevents the strands from shifting out of position under compressive loads, unlike a fiber core which can compress and lead to invisible internal wear.
What does 6x19 or 6x36 mean on industrial wire rope specifications?
These numbers describe the rope's construction pattern.industrial wire rope 6x19 class ropes have six strands with approximately 19 larger-diameter wires per strand, giving them excellent abrasion resistance but more stiffness. A 6x36 class uses many smaller wires per strand, making it more flexible and better suited for applications with small-diameter sheaves or high bending cycles like container cranes.
How should you properly lubricate industrial wire rope?
Use a heavy, penetrating lubricant specifically formulated for wire rope that reaches the core, not just the surface.industrial wire rope Apply it when the rope is warm or slightly stretched on a drum using a roller coater or drip system. Avoid cold grease or improvised substitutes like diesel, which can wash away the manufacturer's internal compound and trap moisture inside.
Why does my wire rope keep twisting or spinning during single-line lifts?
Your rope is twisting because standard 6-strand construction wire ropes naturally unlay under load, transferring torque to the free-suspended load.industrial wire rope You need a rotation-resistant rope, typically built with 8, 19, or 34 strands in layers laid in opposite directions, to neutralize this torsional force and prevent dangerous load spinning during single-part lifts.
Tags:custom coated wire rope | custom wire rope | hanging wire rope
0users like this.
